There is no single best t-shirt printing method. Match it to three constraints: fabric, artwork and order size. Screen printing usually has the lowest unit cost at 100+ pieces for one to three colours, and it is the most durable surface print. DTG and DTF suit runs under 50 pieces and photographic artwork. Sublimation is the method for all-over polyester. Embroidery is for small, solid logos.
The table below compares all 11 methods on fabric, order size, hand feel and wash durability. The sections after it explain how each method fails, so you can specify the right one before a sample is made.
Key facts
| Item | Figure |
|---|---|
| Methods compared | 11 |
| In-house at JaceApparel | Screen printing, all-over sublimation, embroidery |
| Minimum order | 100 pcs per colour |
| Sampling | 7–10 working days |
| Bulk production | 7–15 working days |
| Inspection | AQL 2.5 |
| Print proof | On the production cloth before the bulk run |
The 11 methods at a glance
| Method | Best fabric | Best order size | Hand feel | Wash durability | Best for |
|---|---|---|---|---|---|
| DTF | Cotton, polyester, blends | 1–100 pcs | Medium, film on fabric | Medium | Multi-colour logos on mixed fabrics |
| Plastisol screen | Cotton, blends, some polyester | 100+ pcs | Heavy | High | Bold graphics, Pantone matching |
| Sublimation / AOP | Polyester, high-poly blends | 100+ pcs | None | High | All-over prints, sportswear |
| HTV | Cotton, blends | 1–50 pcs | Medium to heavy | Medium | Names, numbers, one-offs |
| Water-based screen | 100% cotton | 100+ pcs | Soft | High | Premium streetwear, soft-hand prints |
| DTG | 100% cotton, some blends | 1–100 pcs | Soft | Medium | Photos, gradients, short runs |
| Plastisol transfer | Cotton, blends, fleece | 20–500 pcs | Medium | High | Staggered events, stock-light fulfilment |
| Printable transfer | Cotton, blends | 1–20 pcs | Heavy | Low to medium | Samples, one-day events |
| Discharge | 100% cotton, dark shades | 100+ pcs | None | High | Vintage looks on dark cotton |
| Embroidery | Most fabrics, heavier is better | 50+ pcs | Raised thread | High | Small chest logos, polos, outerwear |
| Specialty effects | Cotton, blends | 100+ pcs | Raised or metallic | Medium | Texture, limited editions |
Order-size bands are typical economical ranges, not hard limits. Confirm the break point with the printer, because set-up fees and fabric width move it.
How to read the durability column
These are comparative production judgements, not a lab score or a warranty. Each method fails in a different way: plastisol cracks at the edges, water-based ink fades gradually, DTG fades with washing, and sublimation does not crack because the dye is inside the fibre.
High means the print typically outlasts the garment in normal wear; Medium means visible wear after repeated washing; Low means it is best for short-life items. Treat the bands as a working guide, then confirm the result on your actual fabric.
How to run a wash test
A durability claim is only as good as the test behind it. Use the same fabric, ink, cure and placement as the bulk order, then test to AATCC 61 or ISO 105-C06.
| Checkpoint | What to record | Pass criteria |
|---|---|---|
| 0 washes | Colour, hand feel, edge sharpness | Baseline photo under daylight |
| 10 washes | Edge lift, cracking, fading | No visible cracking or lifting |
| 25 washes | Colour shift, fibrillation | Colour within the approved range |
| 50 washes | Print integrity | Design remains legible and attached |
Photograph the same area at each checkpoint under the same light. A result without a photo and a stated method is an opinion, not a test.
Before a bulk run, ask for a wash test on your fabric to AATCC 61 or ISO 105-C06. The result on your cloth is the only durability figure that matters.
1. DTF (direct-to-film)
How it works. The artwork is printed onto PET film with water-based pigment ink, coated with a hot-melt adhesive powder, cured, then heat-pressed onto the garment. The film bonds to cotton, polyester and blends.
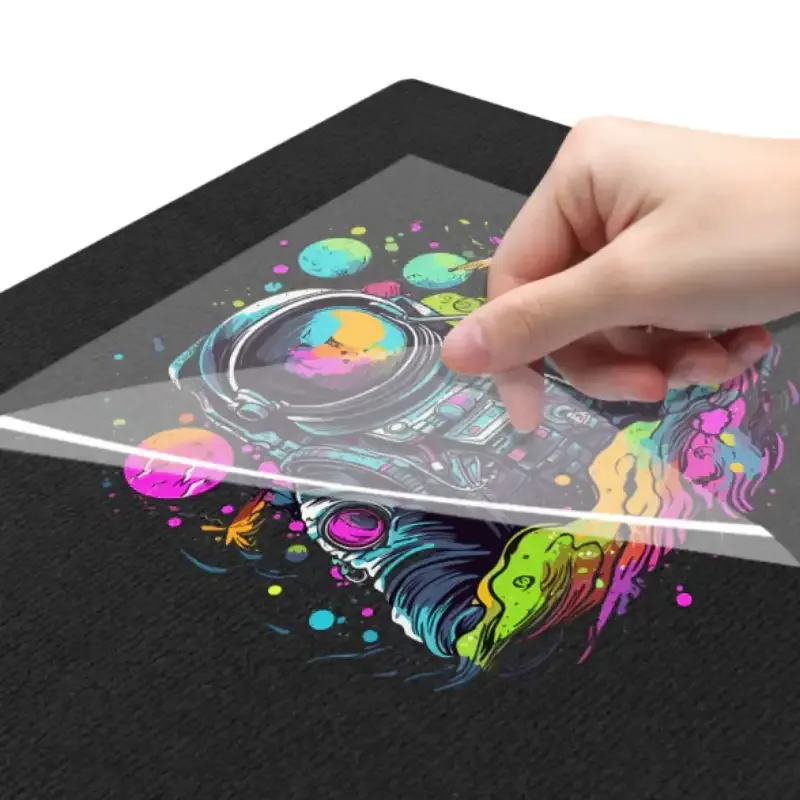
DTF: the design is printed on film, powdered and pressed. The film sits on the surface, so large prints feel heavier.
Best for. Short runs that need identical logos across different fabrics — for example, a drop with cotton tees and polyester hoodies. There is no screen set-up, so the preparation cost is the same at ten pieces or 100; the per-piece cost still falls with volume.
The trade-off. The film sits on the surface. Large back prints reduce breathability and can feel like a sweat patch; edges can lift after repeated washing. Hand feel is heavier than DTG on cotton.
What to specify. Film and powder type, press temperature and time, and a wash test on your fabric. Ask whether the supplier prints on your blank or on a stock blank.
2. Plastisol screen printing
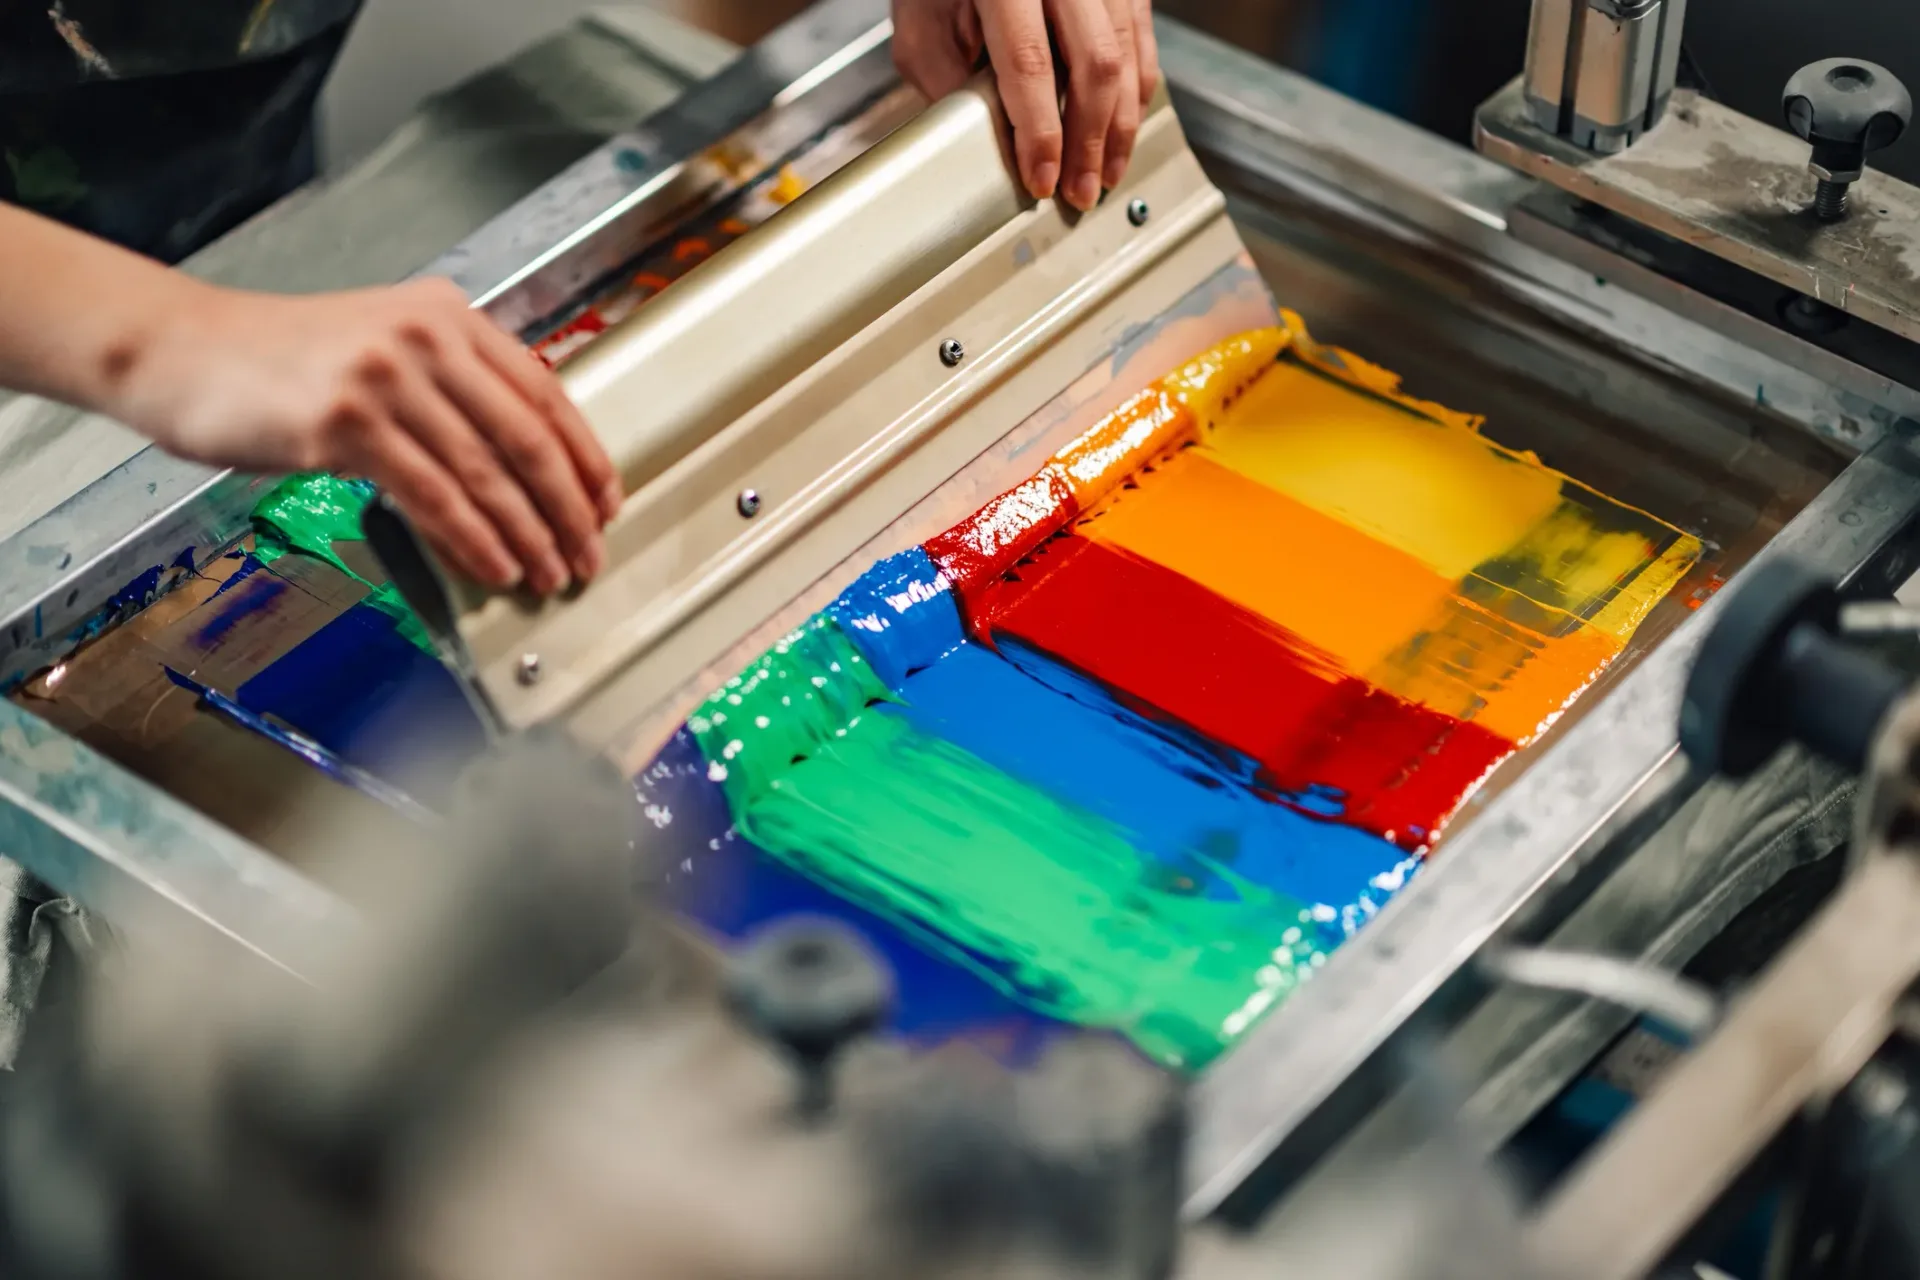
How it works. A mesh screen is coated with emulsion, exposed with the artwork, and ink is pushed through the open areas with a squeegee. Each colour needs its own screen. The ink is cured at roughly 160°C / 320°F.
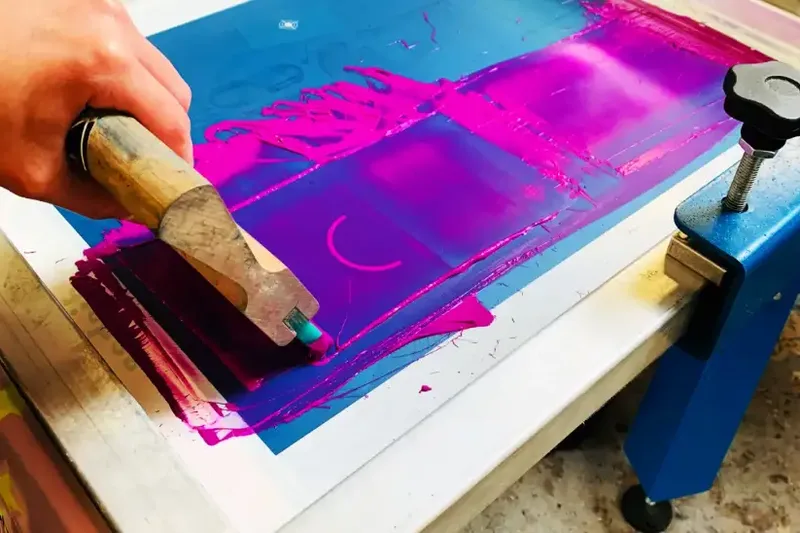
Silk-screen printing: one screen per colour. Registration and cure temperature decide the edge quality.
Best for. Orders over 100 pieces, bold graphics, Pantone matching and dark garments where opacity matters. The set-up cost is spread across the run, so the unit price falls as the quantity rises.
The trade-off. Plastisol sits on top of the fabric, creating a heavier hand. On polyester, standard plastisol can suffer dye migration without a low-bleed ink. Every added colour adds a screen, a set-up fee and registration risk.
JaceApparel note. Screen printing runs in four techniques — silk screen, foil, water-based and puff — plus glow, metallic, discharge and neon inks. The print is proofed on the production cloth before the run.
What to specify. Mesh count, ink type, underbase, cure temperature, flash time and wash standard.
3. Dye sublimation and all-over printing (AOP)
How it works. The design is printed onto transfer paper with disperse dye, then heat-pressed. The dye turns to gas and bonds into polyester fibre, so there is no film on the surface. For all-over printing, the fabric is printed before it is cut and sewn.
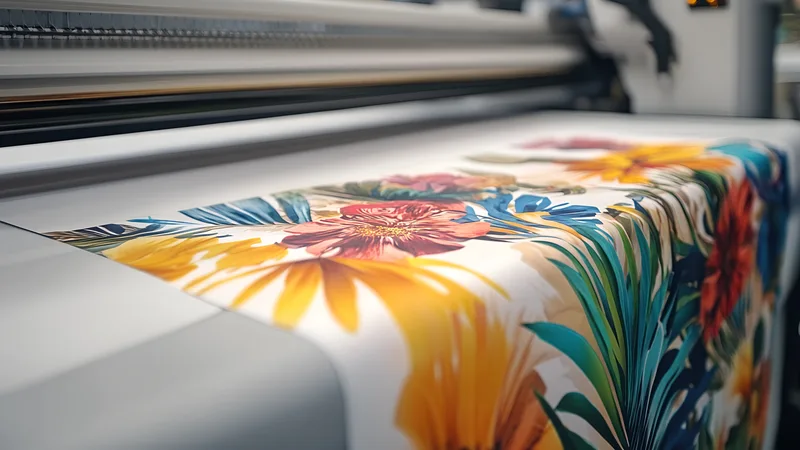
All-over sublimation: the fabric is printed before cutting, so the design can cross seams.
Best for. All-over graphics, sports jerseys, cycling kits and polyester-rich garments. Because the dye is inside the fibre, the print does not crack or sit on the skin.
The trade-off. Polyester only, or high-poly blends. There is no white ink, so a white design on a dark garment depends on the base fabric. Colour on dark polyester shifts, and cotton will not take the dye.
JaceApparel note. Sublimation covers custom pattern, all-over, cut-and-sew and photo sublimation, on a light base.
What to specify. Polyester content, base colour, press temperature and time, paper and colour profile.
4. Heat transfer vinyl (HTV)
How it works. A plotter cuts the design from a vinyl sheet, the excess is weeded away, and the vinyl is heat-pressed onto the garment.
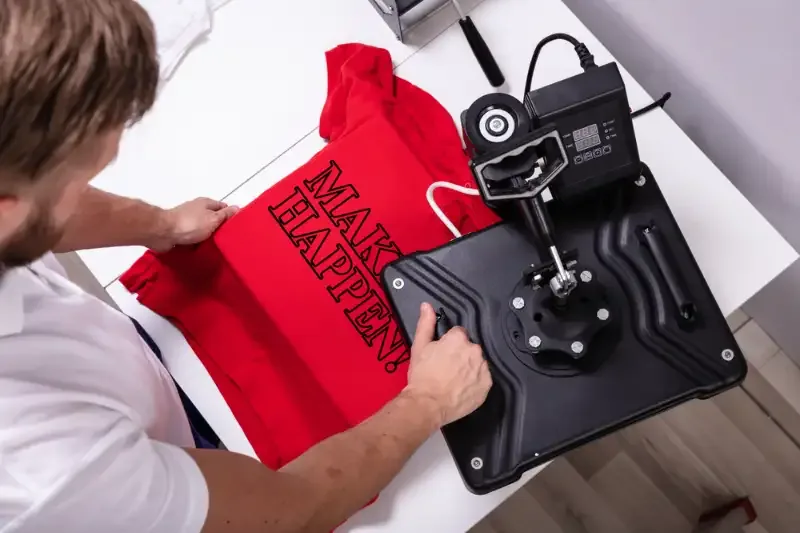
HTV: cut vinyl, weeded and pressed. Sharp corners and large solid areas are the first points of failure.
Best for. Names, numbers, simple vector logos and one-off pieces. It is the fastest way to personalise a small run.
The trade-off. The vinyl sits on top of the fabric. Large areas feel stiff and trap heat, and sharp corners are the first point of failure. It is not suitable for photographs or gradients.
What to specify. Vinyl type (PU or PVC), press temperature and time, peel type (hot or cold) and wash care.
5. Water-based screen printing
How it works. Water-based ink penetrates the fibres instead of sitting on top. On dark cotton, a discharge agent can remove the fabric dye before the pigment is deposited.
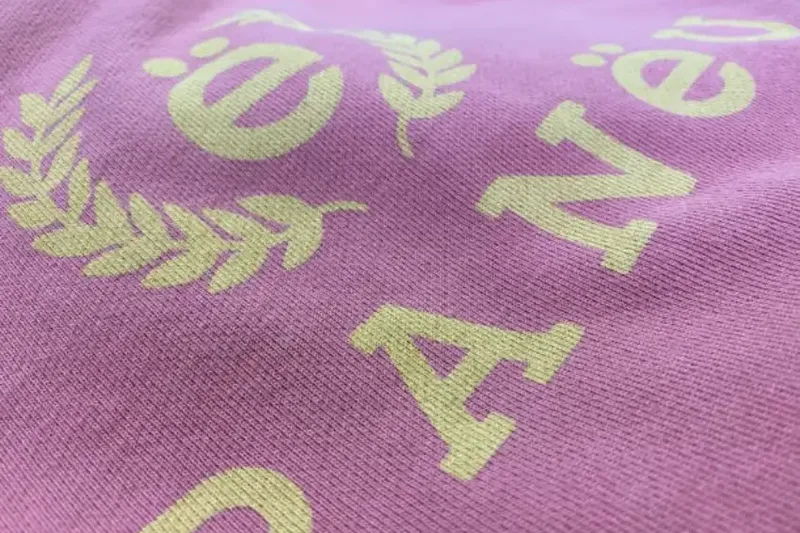
Water-based: the ink soaks into the cotton. The print is soft, but the screen dries quickly and the press runs slower.
Best for. Soft-hand prints on 100% cotton, premium streetwear and any design where the print should feel like the fabric.
The trade-off. The ink dries in the screen, so the press runs slower and stops require cleaning. On dark garments, standard water-based ink is less opaque; discharge changes the colour of the base fabric. Results vary by dye lot.
JaceApparel note. Water-based is one of the four screen techniques. The print is proofed on your cloth, and discharge work starts with a lab dip.
What to specify. Ink system, mesh, cure temperature, discharge versus overprint, and the acceptable colour range.
6. Direct-to-garment (DTG)
How it works. A specialised inkjet printer sprays water-based ink into the fabric. Dark garments need a liquid pretreatment so the white underbase holds; the print is then cured.
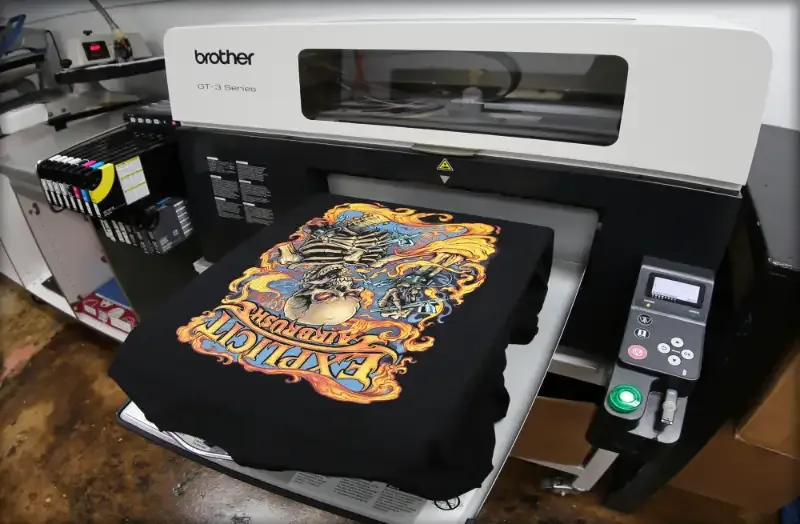
DTG: an inkjet head sprays water-based ink into the fibre. Pretreatment and cure decide whether the print survives washing.
Best for. Photographs, gradients, fine detail and short runs on 100% cotton. There is no screen set-up, so the artwork can change between orders.
The trade-off. Pretreatment and curing decide the result. If either is rushed, the print washes out. Blends and dark garments are harder, and the cost per unit is higher than screen printing at volume.
What to specify. Cotton content, pretreatment, cure temperature and time, print size and resolution, and a wash test.
7. Plastisol transfers
How it works. Plastisol ink is printed onto release paper rather than directly onto the shirt. The sheets are stored, then heat-pressed onto garments as orders arrive.
Best for. Staggered events, sports leagues, touring bands and any order where sizes or names are confirmed late. It separates print volume from garment fulfilment.
The trade-off. Press settings must match the fabric blend; a slight drop in temperature stops the adhesive from curing. The finish sits slightly flatter than direct screen printing.
What to specify. Transfer size, press temperature, time and pressure, fabric blend, and a wash test on the final garment.
8. Printable heat transfers (inkjet and laser)
How it works. The design is printed onto transfer paper and heat-pressed onto the garment. It bypasses screens and films, which makes it the fastest option for one-offs.
Best for. Samples, single-day events and family or team shirts where quantity is low and speed matters.
The trade-off. Quality varies widely. Cheap paper produces a thick plastic film that cracks after a few washes. It is not a retail-grade solution for a brand building repeat customers.
What to specify. Paper type, printer, press settings and a wash test. Ask for a sample that has already been washed, not a fresh press.
9. Discharge printing
How it works. A discharge agent in the ink removes dye from cotton fibres, leaving the pigment or the natural fibre colour. The design becomes part of the fabric rather than a layer on top.
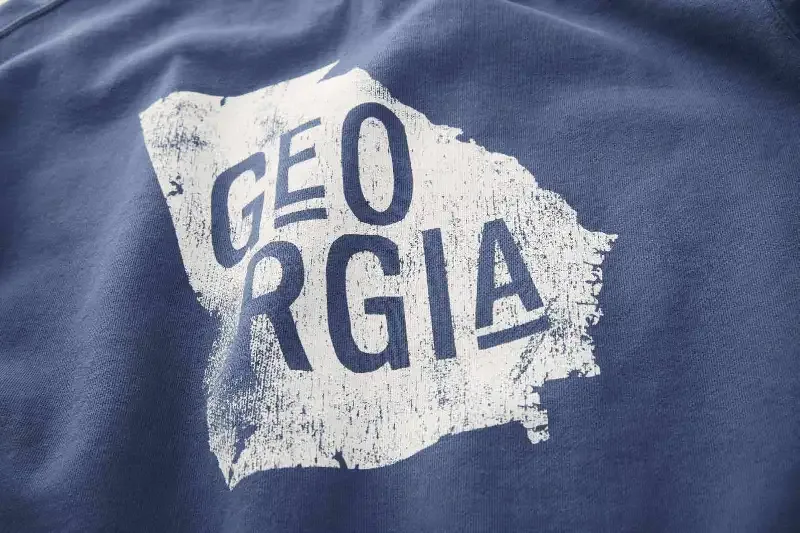
Discharge: the dye is removed before the pigment goes down. The result depends on the dye lot, so a lab dip is essential.
Best for. Dark 100% cotton and a soft, vintage look. It is the softest print on the list because there is no ink film.
The trade-off. Discharge is chemistry, and different dye lots react differently. One black batch may discharge cool grey, another warm brown. Polyester resists the process, and exact Pantone matching is not realistic.
Treat the variation as acceptable only inside a range you approve on a lab dip. Outside that range, it is a defect, not a feature.
JaceApparel note. Discharge is one of the screen inks. Approve a lab dip before the bulk run.
What to specify. Fabric, dye lot, discharge agent, lab dip and the acceptable colour range.
10. Embroidery
How it works. The artwork is digitised into a stitch file and sewn onto the garment by a multi-head machine. The thread sits above the fabric, creating a raised texture.
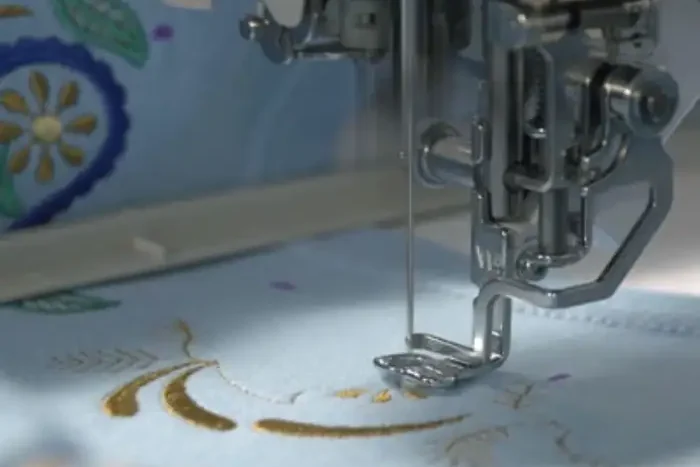
Embroidery: thread, not ink. Solid shapes work; gradients and fine photographic detail do not.
Best for. Small chest logos, polos, caps, outerwear and workwear. Thread does not fade like ink, so the logo often outlasts the garment.
The trade-off. Gradients and photographic detail cannot be stitched. Dense stitching can pucker lightweight fabric, and large logos need a heavier fabric and a stabiliser backing.
JaceApparel note. Custom embroidery is in-house. Keep logos under about 4 inches on a lightweight t-shirt; 200+ GSM cotton handles a larger logo better.
What to specify. Stitch count, thread, backing, needle, placement and artwork format.
11. Specialty screen effects (puff, foil, metallic, glow, neon)
How it works. Additives or foils are added to the screen-print process. Puff ink expands under heat to create a raised surface; foil and metallic inks reflect light.
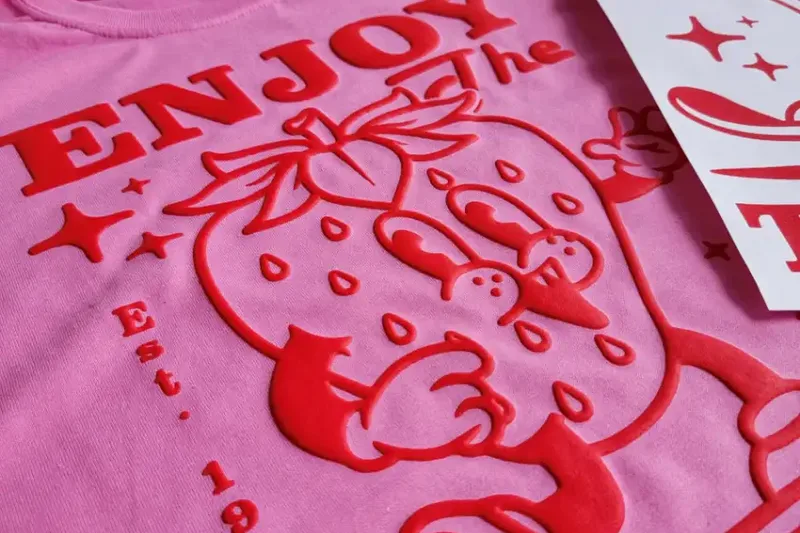
Puff ink raises the print off the fabric. Texture is the product; a physical sample is the only reliable approval.
Best for. Texture, premium drops and limited editions where the print itself is part of the product.
The trade-off. Specialty inks reduce stretch. Thick puff prints crack on tight garments, foil can lift at the edges, and care instructions matter more than for a standard print.
JaceApparel note. Foil, puff, glow, metallic and neon are available as screen effects. Approve a physical sample before the run.
What to specify. Ink system, cure, stretch, wash care and a physical sample.
What drives the cost
The quote is not one number per print. It is a set-up cost plus a unit cost, and the balance changes with the method.
| Driver | Why it moves the price | How to control it |
|---|---|---|
| Set-up | Screens, digitising, films and proofing are one-off costs | Combine artworks; avoid last-minute changes after the proof |
| Colour count | Each screen adds a set-up fee and a registration step | Reduce colours; use DTF for multi-colour short runs |
| Underbase | White ink on dark garments adds a pass and often a surcharge | Print on light garments where the design allows |
| Print area | Large prints use more ink and press time | Keep the print within the planned placement |
| Order size | Set-up is spread over more pieces as the run grows | Commit to a size curve; consolidate colourways |
| Fabric | Weight and composition change ink behaviour and cure | Fix the fabric before choosing the method |
| Finishing | Folding, tagging, polybag and carton add labour | Standardise the pack; print labels in one run |
Ask for the set-up fee and the unit price at 50, 100 and 500 pieces. A quote that gives only one quantity hides the break point where the method stops being economical.
How to choose a method
Work through four questions in order. The first one that rules a method out is usually the decisive one.
- Fabric. 100% cotton: water-based screen, DTG or plastisol. Polyester: sublimation for all-over, DTF or low-bleed plastisol for spot prints. Blends: DTF, or test before committing.
- Artwork. Photographs and gradients: DTG or DTF. One to three spot colours: screen printing. Names and numbers: HTV.
- Quantity. Under 50 pieces: DTG, DTF or HTV. Around 50–100: DTF or DTG, or screen if the design is simple. Over 100: screen printing.
- End use. Workwear: plastisol or embroidery. Premium streetwear: water-based or discharge. Sportswear: sublimation. A one-day event: printable transfer.
Common mistakes
| Mistake | What you see | Prevention |
|---|---|---|
| Low-resolution artwork | Soft or pixelated edges | Supply vector files or a 300 DPI raster at final print size |
| Missing white underbase | Dull colour on dark garments | Specify a white underbase and approve the proof |
| Printing across a seam | Cracks or gaps at the join | Move the placement or print the panel before sewing |
| Under-cured ink | Cracks or washes out early | Measure cure temperature and run a wash test |
| Wrong ink for the fabric | Bleeding, fading or a plastic hand | Match the ink to the fibre; test on the production cloth |
| Approving a digital mock-up only | Colour or hand feel differs from the sample | Approve a physical print on the actual fabric |
Questions to ask a printer
Ask these before paying a deposit. The answers tell you more than a sample photo.
- Do you charge a set-up fee per screen or per colour?
- Is there a surcharge for a white underbase on dark garments?
- What is the maximum print size, and is there a jumbo screen?
- Which wash standard do you test to — AATCC 61 or ISO 105-C06?
- What AQL level do you inspect to, and what is the defect policy?
- Will you proof the print on our fabric, not a stock swatch?
- Who controls pretreatment and curing?
- What are the sampling and bulk lead times?
JaceApparel production parameters
| Item | Figure |
|---|---|
| In-house printing | Screen (silk, foil, water-based, puff, glow, metallic, discharge, neon), all-over sublimation, embroidery |
| Certifications | OEKO-TEX Standard 100, BSCI, GRS |
| Fabrics | Eight working cloths, matched to your target GSM |
MOQ, sampling, bulk lead times, inspection level and proof cloth are listed in Key facts above.
Screen printing, all-over sublimation and embroidery are the methods JaceApparel runs in-house. DTF, DTG, HTV and the transfer methods are included so you can compare a quote or a partner route; they are not presented as JaceApparel floor work.
JaceApparel has made cut-and-sew apparel since 2015, with pattern, cutting, sampling, sewing and finishing in one building. The factory stocks eight working cloths, and the print is proofed on the actual production cloth before the run. See the t-shirt manufacturer page for current capability and the cut-and-sew manufacturer page for the production floor. A recent t-shirt collection case study covers shade consistency from sample to bulk.
How this guide was produced. This guide was written by Yuying Zhu, who has worked in apparel production and sourcing for 16+ years. The method descriptions and trade-offs come from production experience; the JaceApparel parameters come from current production terms. Standards are cited to AATCC, ISO and OEKO-TEX in the Sources section.
Send your fabric, GSM, quantity, print locations and artwork, and we will recommend a method and quote sampling and bulk separately.
Frequently Asked Questions about Types of T-Shirt Printing
01. Which method is best for 50–100 units?
DTF for multi-colour logos on mixed fabrics, DTG for photographs on cotton, and HTV for names and numbers. Screen printing becomes economical at 100 pieces or more, especially for one to three colours.
02. Which printing method is the most durable?
Sublimation and embroidery are permanent because the dye or thread is part of the garment. Plastisol is the most durable surface print. DTG and DTF are lower. The result depends on the fabric and the cure, so test on the production cloth.
03. Screen printing or digital printing — which is better?
Screen printing has a lower unit cost at volume, accurate Pantone matching and strong durability, but each colour adds a screen and a set-up fee. Digital printing (DTG or DTF) has no set-up, handles photographs and short runs, and costs more per unit at volume.
04. What files do you need for an accurate quote?
Vector files (.AI, .EPS or .PDF) or a 300 DPI raster, Pantone references, print placement and size, a quantity breakdown by size, and the fabric or GSM. If you only have a reference garment, the factory can work from that.
05. Can you print on polyester?
Yes, with the right method. Sublimation is the best choice for all-over polyester. DTF or low-bleed plastisol suits spot prints. Discharge and standard water-based inks are for cotton, not polyester.
06. What is AQL 2.5?
AQL is the acceptance quality limit used in ISO 2859-1 sampling. It defines the sample size and the maximum number of defects allowed in a lot. It is a sampling standard, not a zero-defect guarantee.
07. How long does sampling take?
Sampling takes 7–10 working days, then bulk production 7–15 working days. Freight is on top: 5–7 days by air or 30–45 days by sea, plus customs clearance.
08. Do you proof the print before bulk?
Yes. The print is proofed on the actual production cloth — not a stock swatch — before the bulk run. If the fabric changes, the proof is repeated.
09. What is the cheapest printing method for 100 pieces?
For one to three colours on cotton, screen printing is usually the lowest unit cost at 100 pieces because the set-up is spread across the run. For multi-colour artwork or mixed fabrics, compare DTF: it has no screen set-up, but the per-piece cost is higher at volume.
10. Which printing method will not crack?
Sublimation and embroidery do not crack in the way a surface print does: the dye is inside the fibre, and the thread is sewn through the fabric. Plastisol can crack if it is under-cured or stretched; water-based and DTG fade rather than crack. The cure and the fabric decide the result, so wash-test the production cloth.
Sources
- AATCC test methods — colourfastness and wash testing.
- ISO 105-C06 — colour fastness to domestic and commercial laundering.
- ISO 2859-1 — sampling procedures indexed by acceptance quality limit (AQL).
- OEKO-TEX Standard 100 — harmful-substance testing for textile materials.